
Aluminum CNC Milling Design Guide: Optimize Your Parts for Performance and Cost
Designing for CNC milling requires an understanding of how cutting tools interact with aluminum. At CNCALPARTS, we specialize exclusively in aluminum, allowing us to help engineers refine their designs for better stability, reduced cycle times, and tighter tolerance control.
This guide outlines the critical design considerations that help us move your parts from CAD model to finished component efficiently.
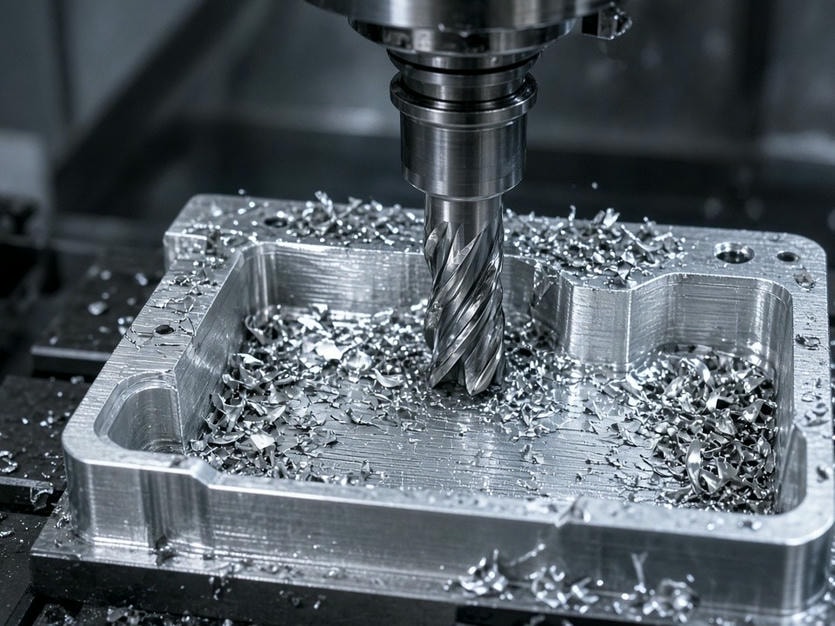
Core Milling Design Principles
To ensure your aluminum parts meet precision requirements without unnecessary cost, consider these geometric guidelines during the design phase.
Internal Corner Radii
Avoid sharp internal corners. Milling cutters are round; a radius at least 30% of the tool diameter allows for faster, more stable machining.
Cavity Depth
Keep depths under 5x the tool diameter. Excessively deep pockets lead to tool deflection and vibration, which compromises surface finish and dimensional accuracy.
Wall Thickness
For structural integrity, maintain a minimum wall thickness of 0.8 mm for small features and 1.5 mm for larger sections. Thinner walls (down to 0.5 mm) are possible but require specialized vibration-dampening techniques.
Holes and Tapping
Standardize hole sizes to match common drill and reamer diameters. For threaded features, ensure enough clearance for chips and avoid blind holes deeper than 3x the diameter.
Workholding Surfaces
Include flat, parallel, or perpendicular faces that allow for secure clamping. If your part is complex, identify which surfaces are cosmetic so we can plan our fixture strategy to avoid clamp marks on critical areas.
Our Aluminum CNC Milling Capabilities
CNCALPARTS operates a dedicated facility in focused solely on aluminum. By eliminating material cross-contamination, we maintain consistent cutting parameters and optimized workholding for high-repeatability production.
Discuss Your Part| Capability | Specifications |
|---|---|
| Milling Axes | 3-Axis, 4-Axis, and 5-Axis |
| Max Milling Size | 1000 × 600 × 500 mm |
| General Tolerance | ±0.05 mm |
| Precision Tolerance | Down to ±0.01 mm |
| Flatness / Parallelism | Down to 0.02 mm |
| Surface Roughness | Ra 0.8–3.2 μm |
| Supported Alloys | 6061, 6063, 6082, 7075, 2024, 5052, 5083 |
Why Specialized Aluminum Machining Matters
General machine shops often balance the needs of steel, titanium, and plastic, which requires frequent changes to machine settings and tooling. Because CNCALPARTS processes aluminum exclusively, our process is tuned for the following priorities.
Deformation Control
Aluminum is prone to stress-induced warping. We use high-speed, light-cut strategies and strategic stress-relief protocols to ensure your thin-wall and large-plate components stay flat.
Surface Finish Consistency
Whether your part requires a bead-blasted matte finish or a high-luster polish prior to anodizing, our tool-path strategies are optimized to minimize tool marks.
Anodizing Readiness
We understand the dimensional shifts associated with anodizing. We adjust our machining tolerances to ensure your parts remain within specification after the coating process.
From Prototype to Batch Production
We support the full product lifecycle. For prototypes, we prioritize fast turnaround and design validation. For low-volume and recurring production, we focus on stable, repeatable setups.
By providing consistent inspection reports—including First Article Reports (FAR) and CMM data—we ensure that your 100th part matches the quality of your first prototype. We work with STEP, SLDPRT, and DXF files to ensure your design intent is perfectly translated into the machine code.
Stage 01
Prototype
Fast turnaround and design validation for new concepts.
Stage 02
Low-Volume Production
Stable, repeatable setups with documented inspection data.
Stage 03
Recurring Batch Production
Consistent quality from first article through repeat orders, with FAR and CMM reporting.
Finishing and Surface Protection
The final look and durability of your component are determined by the finishing process. We provide a range of options to match functional and aesthetic requirements.
As-Machined
Clean, high-quality surfaces direct from the mill.
Anodizing
Clear, black, and custom colors for corrosion resistance and aesthetics.
Hard Anodizing
For high-wear applications in automation and robotics.
Bead Blasting
Provides a uniform, non-reflective finish that hides minor machining marks.
Request a Quote for Your Aluminum Project
If you are currently designing aluminum enclosures, heat sinks, or structural brackets, we are ready to assist. Send your CAD files and technical drawings to info@cncalparts.com.
We review every inquiry for manufacturability before providing a quote. If your design has features that may cause distortion or excessive costs, our engineering team will suggest adjustments to keep your project on budget and on schedule.
CNCALPARTS – We machine aluminum. Only aluminum.
Phone:
Email: info@cncalparts.com
Address: