Deep Pocket Aluminum CNC Machining Services
CNCALPARTS specializes in precision CNC machining for aluminum components. Based in Shenzhen, China, we focus exclusively on aluminum alloys, allowing us to master the specific challenges of high-speed milling, deep pocket machining, and complex geometry control.
We support engineers and procurement teams in robotics, automation, optics, and electronics by transforming 3D models into high-quality machined parts. Whether you require a single prototype or a batch of 500+ production units, our facility is optimized for aluminum.
The Challenges of Deep Pocket Machining
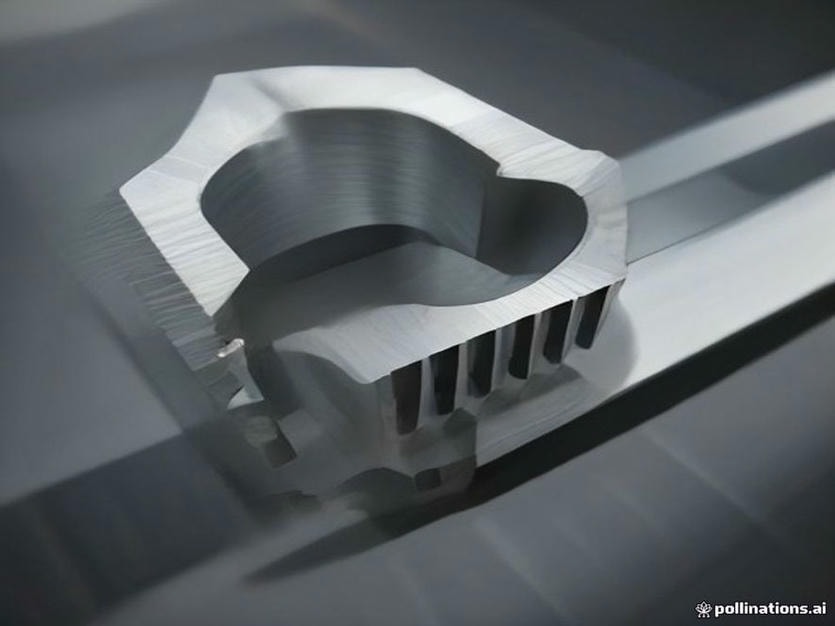
Deep pocket machining in aluminum presents specific technical hurdles that general-purpose machine shops often struggle to manage. When machining deep cavities, we address three primary risks.
Tool Deflection
Long-reach tooling is necessary to reach the bottom of deep pockets. We use high-performance, rigid tool configurations to minimize deflection, ensuring that wall thickness remains consistent and floor flatness meets specifications.
Chip Evacuation
In deep pockets, chips can easily clog the cutting zone, leading to re-cutting, surface scarring, and premature tool failure. We utilize high-pressure coolant systems and specialized tool paths to ensure efficient chip clearance.
Vibration (Chatter)
Deep pockets often result in thin, unsupported walls that are prone to vibration. We manage this through strategic workholding, calculated feed rates, and multi-pass machining techniques to maintain structural integrity and surface finish.
Our Manufacturing Capabilities
Our facility is equipped with 3-axis, 4-axis, and 5-axis CNC machines configured for high-speed aluminum production.
| Capability | Typical Range |
|---|---|
| Primary Material | Aluminum Alloys Only (6061, 6063, 6082, 7075, 2024, 5052, 5083) |
| Max Milling Size | 1000 × 600 × 500 mm |
| Max Turning Diameter | Ø300 mm |
| Tolerance (Precision) | Down to ±0.01 mm |
| Surface Roughness | Ra 0.8–3.2 μm |
| Min Wall Thickness | 0.5 mm |
| Min Hole Diameter | Ø1.0 mm |
| Thread Sizes | M1.6 and above |
Design for Manufacturability Tips
To optimize your deep pocket designs for cost and quality, consider these engineering guidelines. Sensible cavity design lowers machining risk and shortens cycle time.
Corner Radii
Avoid sharp internal corners. A radius of at least 10–15% of the pocket depth allows for larger, more rigid end mills, which reduces cycle time and improves surface finish.
Depth-to-Width Ratio
Extremely deep, narrow pockets are difficult to machine. If possible, design pockets with a width-to-depth ratio that allows for standard tool lengths.
Wall Thickness
For deep pockets, maintain a consistent wall thickness. If walls are too thin, they will deflect during the final passes, leading to dimensional inaccuracies.
Draft Angles
If the part geometry allows, adding a slight draft angle can facilitate tool clearance and reduce the contact area, minimizing heat buildup.
Specialized Aluminum Components
Our focus on aluminum allows us to fine-tune our processes for common industrial applications.
Housings & Enclosures
Precision-fit lids and bases with deep cavities for electronics.
Heat Sinks
Optimized fin spacing and base flatness for thermal management.
Structural Brackets
High-strength 7075 components for automation and robotics.
Optical Mounts
Tight tolerance bores and mounting features.
Manifolds
Complex internal flow paths with high surface finish requirements.
Quality Control and Inspection
Precision requires verification. Every part produced at CNCALPARTS undergoes a rigorous quality control process tailored to the requirements of the drawing.
We utilize CMM (Coordinate Measuring Machines), height gauges, micrometers, and surface roughness testers to verify critical dimensional tolerances, floor flatness and parallelism, wall thickness consistency, and hole and thread precision.
We provide Dimensional Inspection Reports and First Article Reports (FAR) to ensure full compliance with your specifications before shipping.
Verified on Every Run
- Critical dimensional tolerances (±0.01 mm)
- Flatness and parallelism of deep pocket floors
- Wall thickness consistency
- Hole and thread precision
Surface Finishing for Aluminum
We offer in-house and partnered finishing services to ensure your parts meet both aesthetic and functional requirements.
As Machined
Clean, natural finish directly from the CNC.
Bead Blasting
Provides a uniform, matte appearance that hides minor machining marks.
Anodizing
Clear, black, and color anodizing for corrosion resistance and aesthetics.
Hard Anodizing
For applications requiring high wear resistance.
Powder Coating
Durable, decorative finish for exterior-facing components.
The CNCALPARTS Advantage: Aluminum Only
Many shops diversify by machining steel, plastic, and brass alongside aluminum. We do not.
By limiting our scope to aluminum, we maintain a clean environment free from cross-contamination of materials. Our tooling, coolant, and workholding setups are dedicated to the specific physics of aluminum machining. This focus results in faster setup times, better dimensional stability, and consistent anodizing quality.
Faster setup times
Better dimensional stability
Consistent anodizing quality
Request a Quote
We support prototypes, low-volume batches, and recurring production runs. If you have an aluminum machining project that requires precision, deep pocket capability, and reliable delivery, we are ready to review your files.
Please send your STEP/STP files and PDF drawings to info@cncalparts.com.
CNCALPARTS
Phone:
WhatsApp:
We machine aluminum. Only aluminum.